Suitable for
Projects that match this page decision
- Buyers with an approved technical specification and test samples
- Machine orders that need measurable release evidence
- Remote or on-site witnesses reviewing one controlled record
Acceptance execution / measurable factory test
A machine FAT needs an agreed test method and raw results, not only a running video. Define exactly what the rinse-fill-cap monoblock will prove before the witness date, and disclose any temporary equipment or unavailable site conditions.
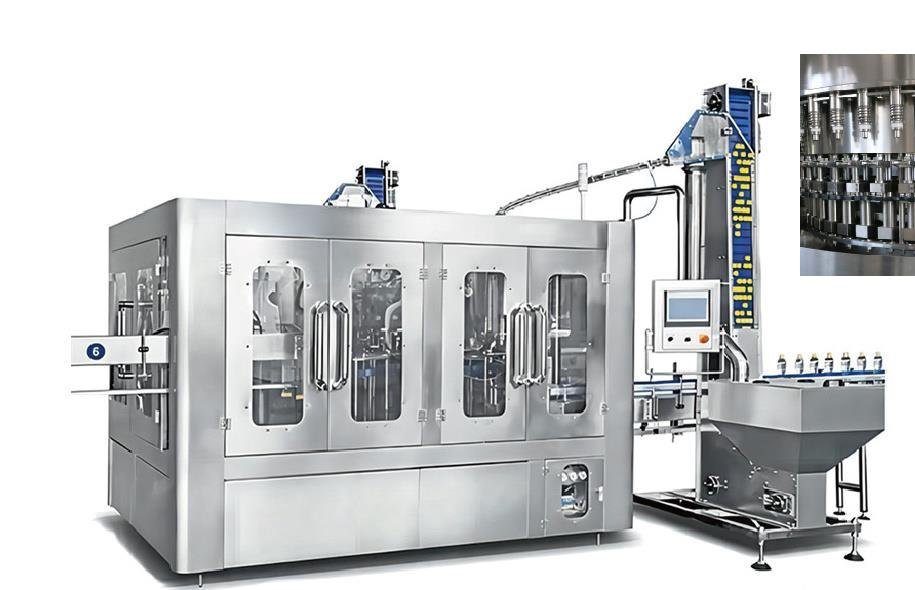
The FAT record should identify the contracted monoblock, approved bottle/cap format and test conditions, then reconcile good output, elapsed time, rejects, stops and quality observations. Failed or deferred checks need named owners, evidence and a defined retest before a recorded release decision.
Record the machine identity, configuration, specification revision, bottle/cap revisions, format parts and settings. Define empty-bottle entry and capped-bottle exit counting points. List test water, utilities, instruments and temporary conveyors. A monoblock test does not prove a labeler, packer, complete-line OEE or conditions absent from the factory.
Agree sample quantities, witnesses, records, run duration and criteria in advance. Qualified supplier personnel perform prescribed dry, protective/control and wet checks under the machine instructions. Record the conditions before the measured run; do not bypass guards or improvise fault tests to obtain a video.
Keep start/end counter readings, elapsed seconds, accepted bottles, rejects and a timestamped stop log on the same run ID. For an elapsed-time rate, good BPH equals accepted bottles times 3,600 divided by agreed elapsed seconds; label any running-time rate separately. Preserve fill, leakage, cap and bottle observations under the agreed methods and limits.
For each failed or deferred check, retain requirement ID, expected result, observation and evidence file. Assign correction owner, date and same-basis retest. Record who decides release and any conditions; a supplier summary cannot silently close an open point. Carry site-dependent checks into the machine commissioning handover, not into a factory-performance claim.
Projects that match this page decision
Boundaries that need a different platform or review
Evidence to provide before confirmation
What happens at this machine or decision boundary
Options that must appear in the proposal
Upstream, downstream and utility handovers
Questions to close before order
How to verify the agreed basis
What the commercial offer should state
No. It can support the record but cannot replace sample identity, agreed criteria, counter/time readings, quality results and stop/reject logs. Remote witnesses need access to the same evidence and unresolved-item list.
No. Use an agreed format/test matrix and record which combinations were actually tested. Untested formats, change parts and output values remain separate confirmation items.
No. FAT applies to the stated factory configuration and conditions. Actual utility connections, machine interfaces and installation-dependent functions still need the agreed commissioning checks at site.
Related decision
Build a practical FAT checklist for PET bottle samples, output, transfer, fill level, leakage, capping, alarms, parts and documents.
Allot Tech / filling-machine-factory-acceptance-test
Send the bottle, cap, reference output, existing equipment and destination. Final values are confirmed in the project proposal.
Mr Kcal
Allot Tech (Suzhou) Co., Ltd.